High Speed HDPE Pipe Machine Advantages for Modern Manufacturing
2026-10-19
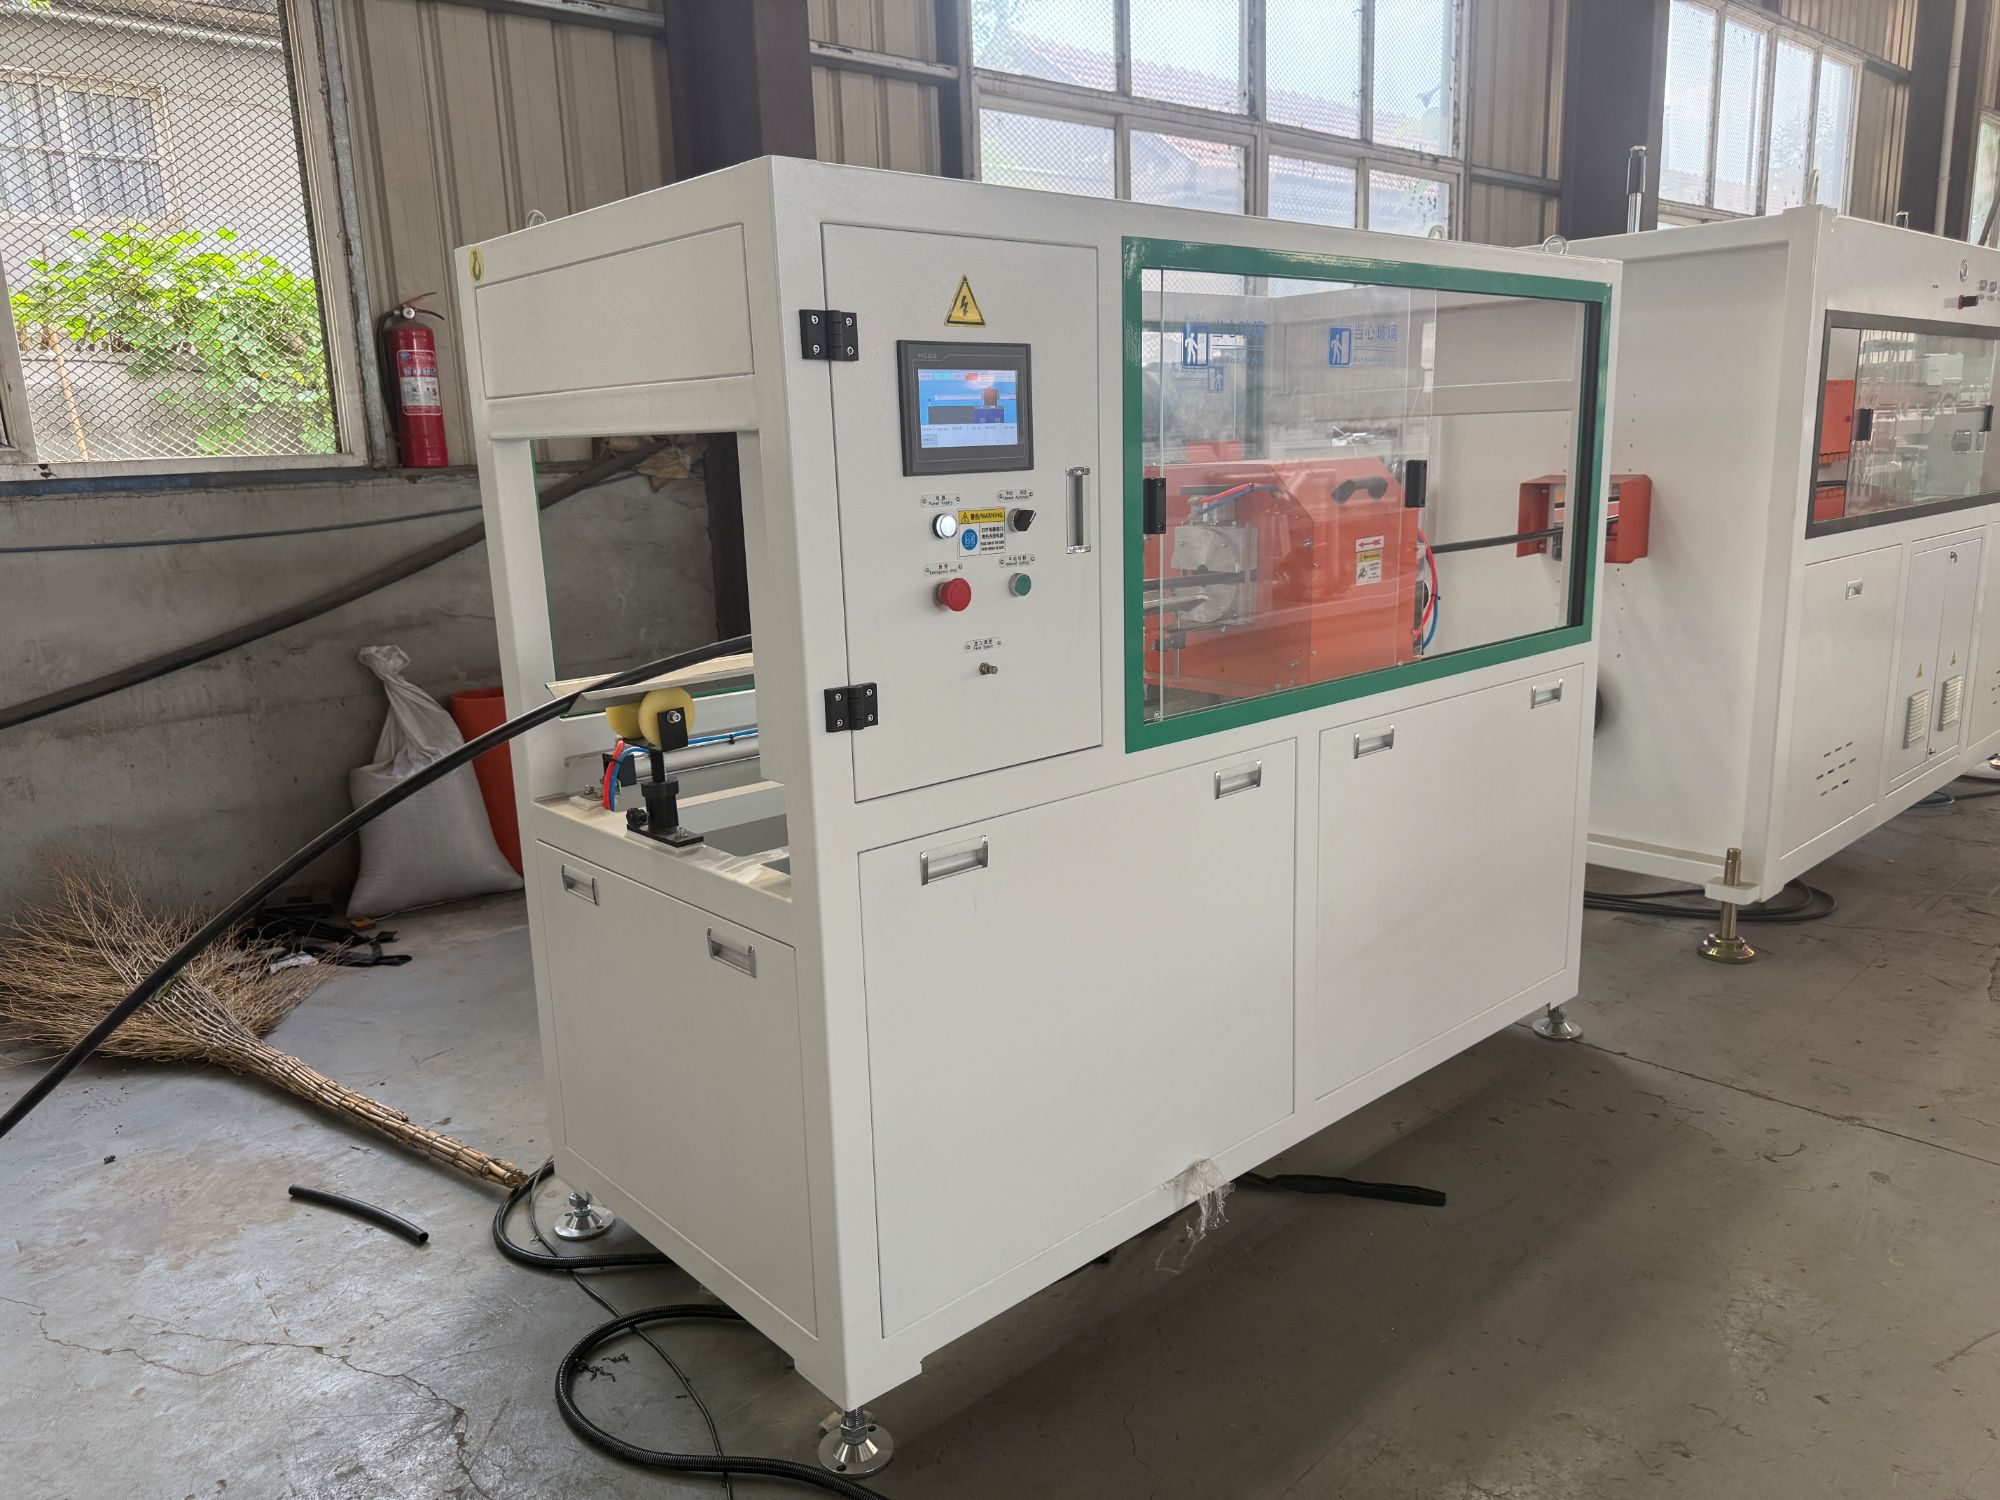
Modern manufacturing never stands still, and for HDPE pipe producers, speed and consistency are no longer optional—they are the baseline. Yet many lines still struggle with uneven wall thickness, high energy consumption, and frequent downtime. High-speed HDPE pipe machines change that equation by combining rapid extrusion with tighter process control. COMRISE has pushed these advantages further, integrating smart temperature management and quick-change dies that slash setup times. As infrastructure demands soar, understanding what truly separates a fast line from a reliable one could be the difference between profit and backlog. Here’s what modern manufacturing actually gains when speed meets precision.
Hitting Output Targets Without Wall Drift
Hitting output targets rarely fails because of a single large error. It fails through wall drift—a slow, almost invisible migration of process settings away from the centerline. Operators compensate for one small variance, then another, until the original recipe is gone and output has quietly slipped. To prevent this, lock the baseline first. Confirm that every sensor, valve, and alignment matches the documented standard before pushing for higher numbers.
A more effective approach separates rate improvements from stability corrections. Increase output by removing material handling delays or smoothing changeovers, not by adjusting process parameters that were already validated. When a shift reports that it “tweaked” a setting to gain a few extra units, treat that as a red flag. The gain looks real in the moment, but it often seeds the next week’s drift.
Short-interval tracking helps, but only if the data is used to reinforce standard work. Compare actual output to the target every hour, and when a gap appears, ask what constraint caused it. Fix the constraint at its source instead of allowing a temporary workaround to become the new normal. A stable line that runs at 95 percent of theoretical maximum will usually outperform a drifting line that occasionally touches 105 percent.
Energy Per Meter Falls as Speed Climbs
At a gentle stroll, each step demands constant micro-corrections just to stay upright. Muscles fire in short, inefficient bursts, and the body spends a surprising amount of energy simply holding itself together. Over a given distance, this adds up to a high energy cost per meter, even though the effort feels light.
Pick up the pace and the picture shifts. Stride length stretches, cadence locks into a smoother rhythm, and tendons start recycling elastic energy like springs. The same distance now costs fewer total joules per meter because the body wastes less on braking and stabilizing. That trend continues until aerodynamic drag or muscular limits eventually push the curve upward again.
Faster Melt Stability Means Fewer Startup Scraps
Startup waste in extrusion rarely comes from bad tooling—it comes from the melt not being thermally settled. When a line fires up, the first several kilograms often carry visible streaking or dimensional drift. A resin that reaches a stable viscosity window in under ten minutes instead of twenty keeps those early shots on spec, not in the regrind bin.
Operators see the difference in purge counts and pressure curves. If the melt index levels off quickly, the feed throat and barrel zones are already pushing a uniform thermal front. That consistency cuts the trial-and-error speed adjustments and lets the first production run match the day-shift standard. Fewer startup scraps also means fewer cleanup cycles and less contamination risk when switching between materials.
Switching Pipe Sizes in Minutes Not Shifts
Traditional pipe size changes mean stopping the line, wrestling with fittings, and losing half a shift to downtime. That kind of interruption doesn't just eat time—it throws off every downstream step. With a system designed for fast swaps, the whole approach changes. Operators can move from one diameter to another while the line keeps moving, using simple locking collars or preset adapters that require no cutting or heavy tooling.
The real gain isn't just speed; it's flexibility. A packaging line that might have been locked into one product run can now shift between formats in a matter of minutes. This turns changeovers from a scheduled headache into a minor adjustment, letting smaller batches and custom orders become practical instead of costly.
From food processing to chemical transfer, the same principle holds: the less time you spend resetting pipe dimensions, the more time you spend producing. When a size change can happen during a brief pause rather than a dedicated shutdown, you stop planning around the changeover and start planning around the output.
The Screw and Barrel Pairing That Survives Downtime
Shutdowns are where many screw and barrel sets quietly fail. Residual polymer breaks down into acidic byproducts, moisture creeps into micro-gaps, and the next startup grinds corrosion debris into the melt stream. A pairing built for downtime uses a high-chromium, nitrided barrel combined with a screw protected by a dense chrome oxide or nickel-based coating. That combination keeps the root clearance stable and prevents pitting from turning a brief idle period into a full rebuild.
Equally important is how the screw flight geometry handles thermal cycling. A slightly deeper feed section with a longer compression zone gives the polymer room to re-melt evenly after a cold start, reducing torque spikes that can gall the barrel wall. Pair that with a barrel liner that has been honed to a consistent surface finish, and you get a unit that comes back online without the usual scrape-and-polish routine. It's less about one magic material, more about matching the two parts so downtime becomes a pause rather than a problem.
Tension Control That Never Needs a Manual Nudge
A tension system that truly runs itself doesn't just hold a setting—it reads the material and reacts before you'd even notice a change. The pull stays consistent whether you're moving fast, slowing down, shifting from thin to thick stock, or working through a slight catch.
That kind of responsiveness removes the little pauses and resets that break your rhythm. You won't find yourself easing a knob back to the right spot or guessing if it's too tight this time. The mechanism does the fine-tuning on the fly, so every pass comes out looking the same.
It's the difference between babysitting a dial and simply getting on with the job. Once you set the starting point, the system keeps the tension in the working zone—no nudging, no second-guessing, and no mid-run corrections pulling your attention away.
FAQ
By employing twin-screw extrusion and vacuum calibration, these machines can sustain output of several hundred kilograms per hour while keeping wall thickness consistent, allowing a single line to replace two conventional lines.
Their ability to switch between pipe diameters quickly with minimal tooling changes and built-in process monitoring reduces downtime and scrap, fitting lean production schedules.
Advanced barrel heating zones with ceramic heaters and insulated covers, plus optimized screw geometry, cut specific energy use per kilogram of pipe by up to 15% compared to older models.
Automated temperature control, diameter adjustment, and fault diagnostics let one operator supervise multiple lines, reducing labor costs and human error during long runs.
Closed-loop control of melt pressure and haul-off speed, combined with multi-sensor wall thickness measurement, keeps ovality and thickness within tight tolerances even at maximum throughput.
Most manufacturers see payback within two to three years due to higher output, lower scrap rates, and reduced energy bills, though this depends on local resin and labor costs.
Quick-change dies and adjustable vacuum tanks allow diameter transitions in under an hour, making short production runs economically viable without sacrificing output consistency.
Conclusion
Modern extrusion lines often chase higher throughput at the cost of wall consistency, but the latest high-speed HDPE pipe machines flip that trade-off. Closed-loop thickness control tied directly to haul-off speed lets operators push line rates well past legacy ceilings without the usual drift in wall thickness. The energy story changes too: because output climbs faster than the proportional power draw, the cost per meter actually drops as speed increases. On startup, the extruder reaches a stable melt condition more quickly, so the initial pipe that would normally be scrapped becomes usable product almost from the first meter.
Beyond steady-state performance, changeovers and long-term wear separate these machines from older generations. Pipe diameter and wall adjustments no longer require half a shift of manual calibration; the downstream sizing and cooling modules reposition themselves and the line re-centers in minutes. The screw and barrel combination is engineered to tolerate the inevitable stops and reheats without rapid degradation, protecting throughput months down the road. Meanwhile, the tension control monitors reel pull automatically and adjusts in real time, eliminating the manual nudges that used to cause ovality or surface marking on thin-wall HDPE pipe.
Contact Us
Contact Person: LISA LEE
Email: [email protected]
Tel/WhatsApp: +86 13780696467
Website: https://www.qdpipemachine.com