Top PPGI Coil Options for Durable Roofing and Wall Panels
2026-10-09
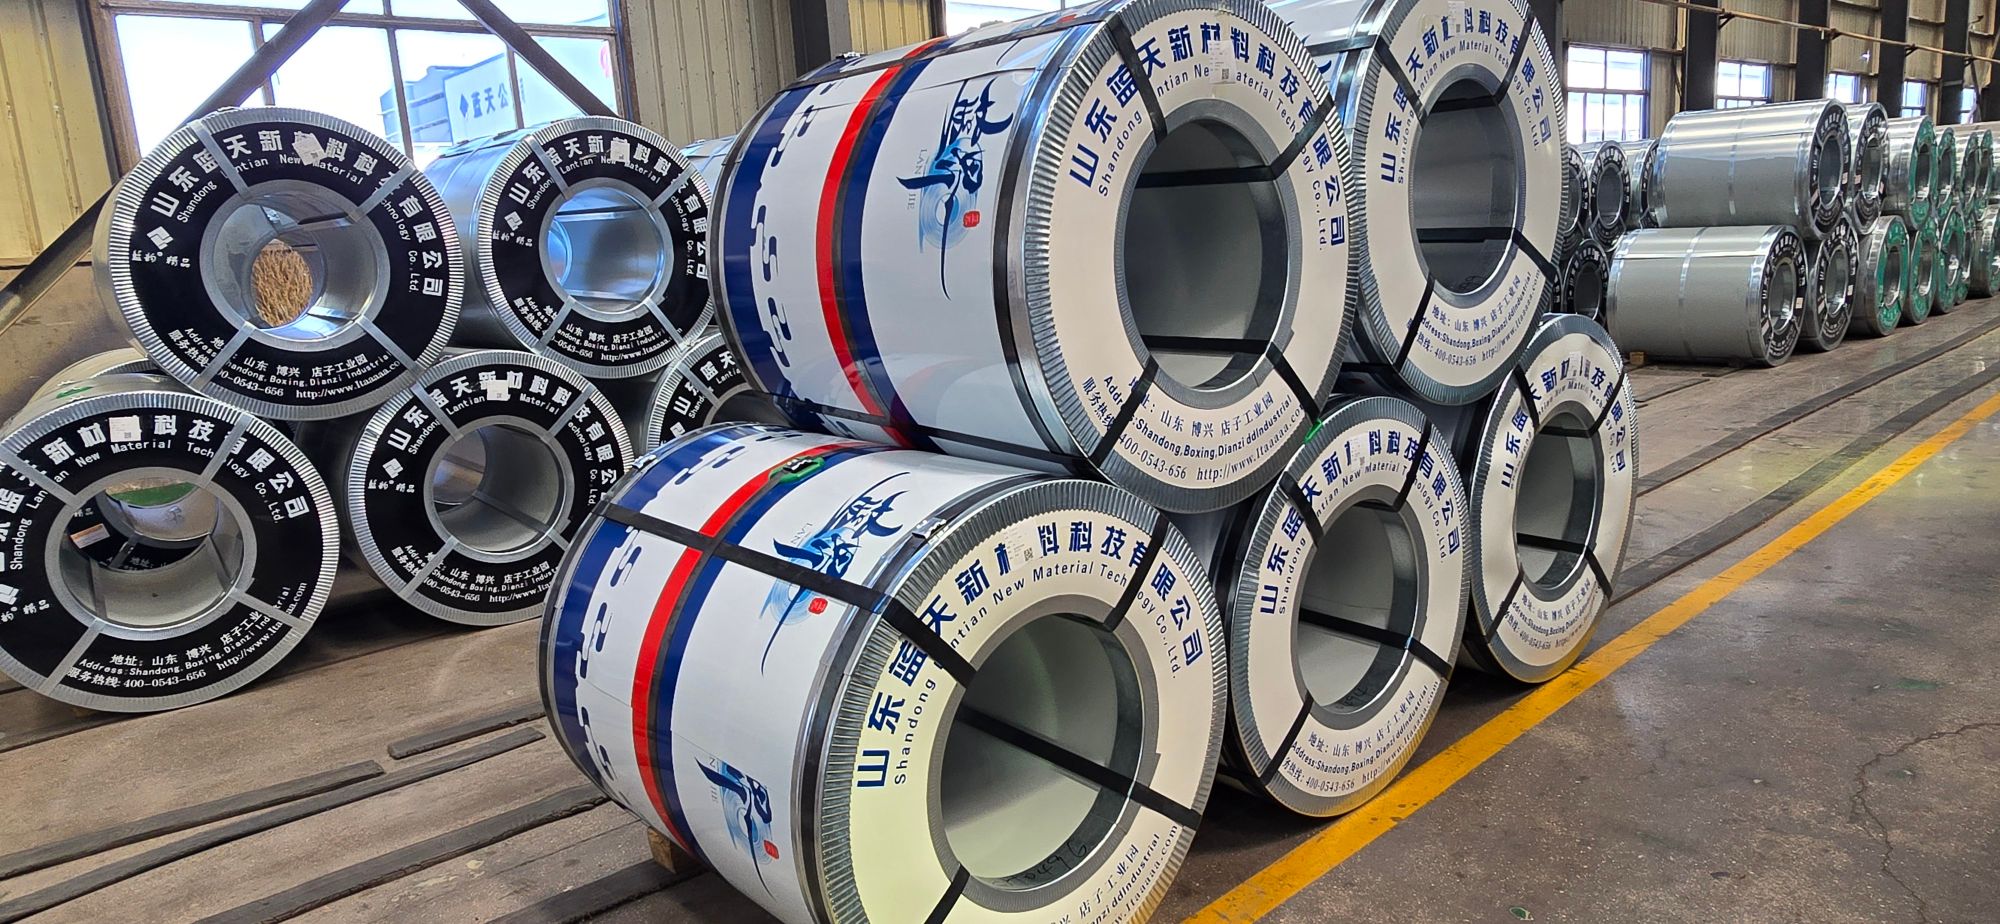
You could assume all PPGI coils are alike—until your roof starts rusting in year three. The truth is, not every pre-painted galvanized coil is built for the long haul. Coating type, primer layer, and base metal quality separate a 20-year panel from a costly redo. In this post, we break down the top PPGI coil options for durable roofing and wall panels, focusing on what actually matters on a job site. One name that consistently delivers on those specs is LANYUN. But don't take our word for it—here's how to evaluate the options yourself.
Start with the Right Galvanized Base—Not All Steel Is Equal
The phrase "galvanized steel" gets thrown around like it’s a single, uniform product, but the base metal underneath the zinc coating decides how the finished piece behaves in the field. Cheap imports often start with recycled scrap that carries unpredictable levels of phosphorus, sulfur, and silicon—elements that quietly weaken the bond between steel and zinc. When that bond fails, the coating flakes away in sheets, leaving bare patches that rust within a season. A proper galvanized base uses controlled chemistry, usually drawing from virgin iron ore or tightly sorted scrap, so the steel’s surface accepts zinc evenly and holds it under thermal stress.
You can spot the difference before the first cut if you know what to look for. Run a finger along a sheared edge: high-quality galvanized sheet shows a clean, silvery line where the zinc has smeared into the steel, while low-grade material often reveals a ragged, gray boundary with visible pinholes. The thickness of the zinc layer matters, too—G90 and G60 are not interchangeable when you’re building something that will sit outdoors for decades. G90 gives roughly 0.9 ounces of zinc per square foot, nearly 50% more than G60, and that extra mass buys years of corrosion resistance in humid or coastal environments.
Then there’s the question of how the galvanizing is applied. Hot-dip galvanizing produces a metallurgical bond with distinct iron-zinc alloy layers that can take a beating; electrogalvanizing lays down a thinner, more uniform coating that looks pretty on indoor fixtures but struggles outside. Some fabricators try to pass off the latter as a budget substitute, and it fails exactly where you need it most: at cut edges, punched holes, and weld points. If the base steel isn't clean, smooth, and properly pretreated, even the best zinc bath won't save it—the coating will simply slide off under a scratch. Start with the right base, and every downstream decision gets easier.
Why Some Colors Fade Faster Under Harsh Sunlight
Why some colors fade faster under harsh sunlight comes down to photodegradation and pigment chemistry. When ultraviolet photons hit a dyed surface, they carry enough energy to break the chemical bonds that give a color its particular hue. Reds and yellows often fade more quickly because the organic compounds used to produce those shades—azo dyes and certain carotenoid-like structures—have double bonds that are especially vulnerable to UV attack. Blues and greens, on the other hand, frequently rely on more stable phthalocyanine or mineral-based pigments, which can absorb and dissipate UV energy without falling apart as quickly.
But the substrate matters too. A fabric or paint base that contains titanium dioxide, often added for brightness or opacity, can accelerate fading by acting as a photocatalyst. When UV light strikes titanium dioxide, it generates reactive oxygen species that attack the colorant molecules nearby. That's why a bright yellow cotton shirt left in direct summer sun can look washed out within a few weeks, while a similarly exposed blue polyester jacket retains much of its original depth. Humidity and heat worsen the process, since higher temperatures speed up the chemical reactions and moisture helps create free radicals.
There's also a perception factor: some colors simply show loss of saturation more obviously. A slight shift in a vivid red or orange is immediately noticeable because those hues sit in the middle of the visible spectrum where human eyes are most sensitive to changes in chroma. A faded navy or forest green might lose the same percentage of dye, yet still appear acceptable because our visual system tolerates dark desaturation better. Manufacturers often add UV absorbers or stabilizers to slow the damage, but ultimately, the combination of pigment chemistry, substrate reactivity, and human vision decides which colors surrender first under relentless sunlight.
Matching Coatings to Coastal or Inland Environments
Coastal settings throw a mix of salt spray, high humidity, and intense UV at any coated surface. The real challenge isn't just the visible rust on railings, but the way chloride ions sneak under paint films at edges and fasteners, driving corrosion outward even when the surface looks intact. For these areas, a high-build zinc-rich epoxy primer paired with a tough polyurethane topcoat makes sense, because the zinc sacrifices itself while the topcoat blocks moisture and sunlight. Avoid thin single-coat systems; they simply don't hold up against constant wet-dry cycling near the shoreline.
Inland environments have their own quiet aggressors. Industrial zones may carry sulfur dioxide and nitrogen oxides, leading to acid rain and micro-pitting, while rural high-altitude sites see intense UV without the salt. Here, the coating choice often shifts away from zinc-heavy systems toward acrylic or polyurethane finishes that can handle chemical exposure and wide temperature swings. But don't assume inland means easy: freeze-thaw cycles, airborne dust, and prolonged condensation under bridges can be just as demanding as coastal fog.
The most practical approach is to map the specific stressors of the site rather than choosing a generic "coastal" or "inland" product. Check shaded north-facing walls, areas under eaves, or spots near exhaust vents—these microclimates can behave differently from the overall region. A coating that works perfectly on a sunny coastal facade may fail quickly inside a shaded car park, and a product designed for dry inland air may blister in a foggy river valley. Periodic inspections and small patch tests help fine-tune the match before a full repaint.
The Hidden Impact of Coil Grain Direction on Panel Life
Most stamping lines run coil after coil without ever checking how the grain lies relative to the bend. That oversight shows up later as microcracks along the outside radius or premature fatigue in panels that flex during service. The grain structure in rolled sheet metal stretches in the rolling direction, and the material’s ductility across that direction is considerably lower. When a brake press folds a panel with the bend axis running parallel to the grain, the outer fibers must stretch across the elongated grains. They tear sooner, and the resulting surface defects act as stress risers from day one.
The difference is not theoretical. Two blanks cut from the same coil can behave like different materials depending on rotation. A panel bent perpendicular to the rolling direction typically accepts a tighter radius without cracking and holds up longer under repeated loading. In fatigue testing, cracks tend to propagate more readily along the aligned grain boundaries, so a panel whose major stress cycle runs across the grain will develop visible cracks earlier than one where the load path follows the rolling direction. This hidden variable often explains why one batch of panels survives years while another batch from the same spec fails in months.
Tooling and part designers rarely flag grain direction on drawings, but the ones who do save themselves from field failures. A simple note calling for the bend line to run perpendicular to the rolling direction can add significant life to a panel with no extra material cost. In some shops, nesting software rotates parts to maximize sheet usage, unintentionally placing the worst grain orientation on high-flex areas. Checking the coil certification and aligning the blank with the grain becomes a low-cost way to avoid warranty claims that otherwise would be blamed on material quality.
Primer Systems That Hold the Topcoat in Place
The main job of a primer is not just to fill imperfections; it creates a bond line that locks the topcoat onto the substrate. A high-quality primer system works on two fronts: it chemically bites into the surface below and provides a textured, porous layer for the topcoat to mechanically cling to. Without this anchoring layer, topcoats tend to peel, chip, or flake under thermal cycling or moisture exposure.
Among the most reliable anchoring primers are acid-etch formulations for bare metal, which use phosphoric or chromic compounds to micro-roughen and passivate the surface. Epoxy primers offer exceptional grip on fiberglass, aluminum, and existing finishes because they cross-link into a dense, waterproof barrier that topcoats can sand into. Urethane primers sit between etch and epoxy in terms of adhesion and flexibility, often chosen when the topcoat will face frequent flexing or impact.
To keep the topcoat locked down, the primer must be applied within the system's recommended film thickness. Too thin and you lose the mechanical key; too thick and the primer can shrink or crack under the topcoat. Light scuffing with the correct grit before topcoating creates thousands of tiny scratches that increase surface area for bonding, while a tack rag removes dust that could act as a release agent. Letting each primer coat flash off completely before the next application prevents solvent entrapment, which is a common cause of topcoat delamination.
Oiling, Passivation, and Other Finishing Touches
A light oil film does more than prevent rust on machined surfaces—it keeps threaded holes from galling during assembly and gives bare steel a consistent sheen that clients notice right away. We usually wipe on a thin coat of ISO VG 32 or a dedicated metal protectant, then buff off the excess so parts don’t attract dust on the shelf.
For stainless and aluminum, passivation or anodizing changes how the surface behaves under handling and humidity. Citric or nitric passivation removes free iron and lets the natural oxide layer rebuild evenly, which matters more on laser-cut edges and tapped bores than on flat faces. A quick water-break test tells us whether the chemical treatment actually took.
Small finishing touches often separate a good run from a rework order. We deburr sharp corners, mask press-fit bores before coating, and add a dry-film lubricant where customers will slide mating parts by hand. These steps aren’t glamorous, but they make the difference between a part that feels unfinished and one that’s ready to install.
FAQ
PVDF (often sold as Kynar 500 or Hylar 5000) remains the top performer for exterior roofing and wall panels. It resists chalking, fading, and chemical breakdown far longer than standard polyester or even SMP. In harsh UV environments, a 70% PVDF formula with ceramic pigments will keep its color and gloss for decades, while lower-cost polyester coatings may show visible dulling within a few years.
For coastal or high-salt environments, a galvalume substrate (55% aluminum-zinc alloy) generally offers better cut-edge protection and longer service life than plain galvanized. However, if the project uses heavy forming or deep profiles, galvanized may bend more forgivingly. Match the substrate to the panel profile and exposure, not just the price.
A total dry film thickness of 25–35 microns on the top side is common for commercial roofs and walls. That usually includes a 5–7 micron primer plus a 20–28 micron topcoat. Thicker isn't always better; if the coil is roll-formed into tight profiles, excessive thickness can crack or delaminate. Ask for the primer and topcoat breakdown, not just the total.
Yes. Solar reflective pigments and cool-roof formulations are available in many colors beyond white. These coatings reflect more infrared radiation while still delivering deep or dark shades. Look for total solar reflectance (TSR) values and emissivity ratings if energy performance matters. A dark brown panel with IR-reflective pigment can stay noticeably cooler than a conventional dark brown panel.
Standard polyester is affordable and fine for interior or mild exterior use, but it tends to chalk and fade faster outdoors. SMP (silicone-modified polyester) adds silicone resin, improving gloss retention and weather resistance at a mid-range cost. For walls that face direct sun but don't justify the cost of PVDF, SMP is often the practical sweet spot.
Many mills offer embossed, matte, wrinkle, or wood-grain finishes. These textures can hide oil canning, fingerprints, and minor surface imperfections better than high-gloss smooth finishes. Matte and textured coatings may also have slightly different cleaning and weathering behavior, so request outdoor exposure data for the specific finish rather than assuming it performs like a gloss product.
The backer coat protects the reverse side from moisture, condensation, and minor abrasion during transport, roll forming, and installation. For roof and wall panels, a 5–10 micron epoxy or polyester backer is standard. Skipping it can lead to white rust or corrosion on the hidden side, especially in humid or coastal climates, so it's rarely worth omitting.
Depends heavily on coating chemistry, pigment type, and exposure. A premium PVDF coating with inorganic pigments can often go 25–35 years before noticeable fade exceeds 5 Delta E units. A standard polyester may show obvious change in 5–10 years. Ask for accelerated weathering test results (like QUV or Xenon arc) as a rough guide, but understand that real-world results vary by orientation, rainfall, and pollution.
Conclusion
Selecting the best PPGI coil for roofing and wall panels starts well before the color is applied. The galvanized base matters more than many buyers realize—different grades of steel hold zinc differently, and a weak foundation will crack or corrode long before the topcoat fails. From there, pigment chemistry decides whether the panel keeps its color under intense UV exposure or turns chalky within a few seasons. Coastal and inland sites cannot use the same coating system: salt spray and high humidity demand a thicker, more flexible primer, while dry inland conditions reward harder finishes that resist abrasion. Even the direction of the coil grain changes how the panel flexes during installation, and cutting against it can invite micro-fractures that shorten service life.
Once the topcoat is chosen, the hidden layers decide durability. A quality primer does not merely sit under the paint—it locks the topcoat to the metal, absorbing stress from thermal movement and preventing underfilm corrosion. Finishing touches like chromate-free passivation and controlled oiling stop white rust before the panel leaves the warehouse, yet too much oil can interfere with adhesive bonding on site. The top PPGI coil options therefore combine a proven galvanized substrate, a UV-stable pigment system matched to the local environment, a primer engineered for the specific climate, and a surface treatment that protects without contaminating. Skipping any one of these steps saves money early but guarantees a shorter panel life and a much higher replacement cost later.
Contact Us
Contact Person: Nia
Email: [email protected]
Tel/WhatsApp: +86 18954360337
Website: https://www.sdppgi.com