How Do You Maintain a Wire EDM Chuck for Precision Workholding for Long-Term Accuracy
2026-09-30
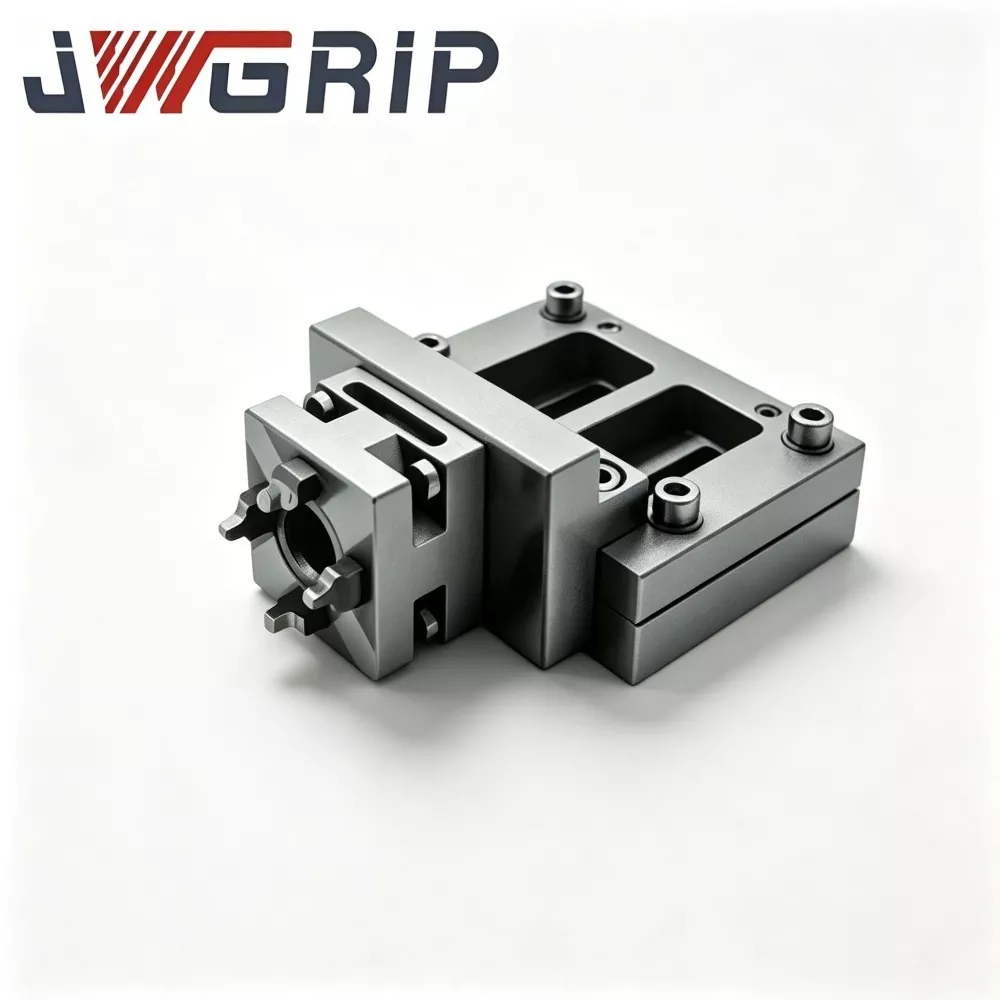
Maintaining a Wire EDM Chuck for Precision Workholding is not a one-time task; it is a disciplined process that directly determines whether your machine holds microns or drifts into scrap. At JWGRIP, we have seen shops lose accuracy not because their wire EDM was worn out, but because their workholding was neglected. A Wire EDM Chuck for Precision Workholding from JWGRIP is engineered for stability, but even the best system requires structured care to deliver long-term repeatability.
Why Maintenance Determines Accuracy
Wire EDM cutting forces are low, but thermal cycling, dielectric fluid contamination, and micro-debris still affect chuck performance. The primary goal is to preserve the clamping reference surfaces and the electrical contact integrity that a Wire EDM Chuck for Precision Workholding depends on. When these degrade, part position shifts, and taper errors appear.
Daily Maintenance Checklist
| Task | Purpose | Frequency |
|---|---|---|
| Wipe clamping surfaces with lint-free cloth | Remove dielectric residue and micro-particles | Every shift |
| Check air/oil lines for leakage | Maintain consistent clamping pressure | Daily |
| Inspect jaw tips for wear or burrs | Prevent part indentation and misalignment | Daily |
| Verify chuck zero position with a test pin | Confirm repeatability before production | Daily |
Weekly and Monthly Procedures
| Interval | Action | Expected Outcome |
|---|---|---|
| Weekly | Clean internal coolant channels and blow out debris | Stable thermal behavior |
| Weekly | Check mounting bolts with a torque wrench | No vibration-induced drift |
| Monthly | Measure clamping force with a load cell | Detect spring or hydraulic fatigue |
| Monthly | Inspect electrical grounding contacts | Reliable EDM signal transfer |
| Quarterly | Re-lap reference surfaces if flatness exceeds 2 µm | Restored precision |
JWGRIP Recommended Best Practices
-
Never clamp a part without cleaning both the Wire EDM Chuck for Precision Workholding surfaces and the workpiece.
-
Use a torque-limited driver when adjusting jaw pressure to avoid over-compression.
-
Keep a maintenance log with dates, measurements, and operator initials.
-
Replace worn jaw inserts before they affect part geometry.
-
Store spare JWGRIP components in a clean, dry environment.
Common Causes of Accuracy Loss
| Symptom | Likely Cause | Corrective Action |
|---|---|---|
| Part-to-part variation | Debris on clamping surface | Clean and re-zero |
| Tapered cut | Chuck misalignment | Re-calibrate with dial indicator |
| Poor surface finish | Grounding contact wear | Replace contact pins |
| Clamping force drop | Seal or spring fatigue | Service hydraulic/pneumatic unit |
FAQ: Wire EDM Chuck for Precision Workholding
How often should I calibrate a Wire EDM Chuck for Precision Workholding?
Calibrate monthly under normal use, or weekly in high-volume production, using a certified test pin and dial indicator to verify repeatability within 1–2 µm.
What cleaning solution is safe for a Wire EDM Chuck for Precision Workholding?
Use a non-corrosive, dielectric-compatible cleaner, then dry with lint-free cloth; avoid chlorinated solvents that can damage seals and coatings.
Can I repair a worn Wire EDM Chuck for Precision Workholding in-house?
Minor jaw replacement and surface cleaning are suitable in-house; however, reference surface re-lapping and hydraulic service should be performed by JWGRIP or a certified technician to maintain accuracy.
When to Replace vs. Service
If runout exceeds 5 µm after calibration, or if clamping force drops below 80% of specification, replacement is more cost-effective than repeated service. JWGRIP supports both paths with genuine parts and technical guidance.
Protect your precision investment with expert support from JWGRIP. Contact our team today for maintenance kits, calibration service, and genuine replacement components for your Wire EDM Chuck for Precision Workholding. Let JWGRIP help you achieve long-term accuracy and zero-defect production.
