How Does Surface Treatment Improve Hydraulic Cylinder Corrosion Resistance?
2026-09-24
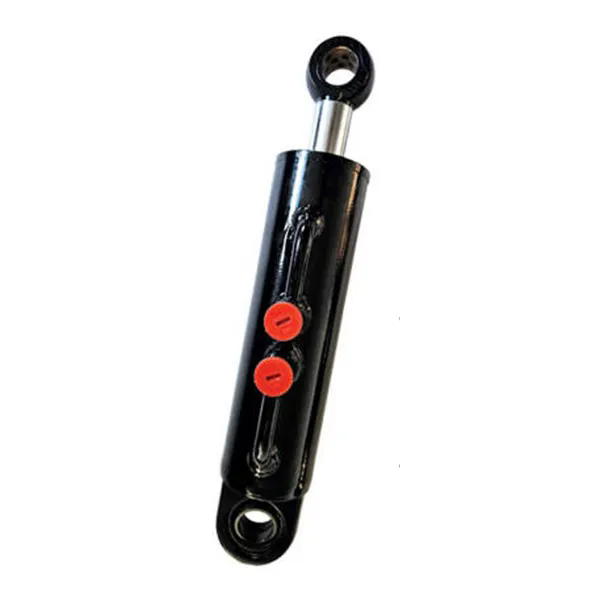
When a Hydraulic Lift Cylinder fails in a coastal or humid environment, the failure almost always starts at the piston rod surface. The rod is the only part of the cylinder that is exposed to the atmosphere, and it is also the part that slides through the rod seal thousands of times per day. The combination of moisture, salt, and abrasion creates a perfect storm for corrosion. The first sign is a small pit or a dull spot on the chrome surface. That pit becomes a stress riser, which leads to micro-cracking. The micro-cracks grow, and eventually the chrome layer flakes off. Once the chrome is gone, the underlying steel corrodes rapidly, and the rod seal is destroyed by the rough surface. This guide explains how surface treatment prevents this failure chain and how to select the right treatment for your operating environment.
1. What Are the Stages of Corrosion Failure on a Hydraulic Lift Cylinder Rod?
Corrosion failure on a Hydraulic Lift Cylinder rod does not happen overnight. It progresses through four stages. The first stage is pit initiation. A small defect in the chrome layer, or a chemical attack from chloride ions, creates a local corrosion cell. The pit is typically 0.05 to 0.2 mm in diameter and 0.02 to 0.05 mm deep. The second stage is pit growth. The pit deepens and widens as the corrosion continues. The edges of the pit become sharp, which creates a stress concentration. The third stage is crack initiation. The stress concentration at the pit edge exceeds the fatigue limit of the chrome layer, and a micro-crack forms. The fourth stage is spalling. The crack propagates along the interface between the chrome and the steel, and a piece of chrome flakes off. The table below shows the time to each stage in a salt spray environment.
| Failure stage | Visual appearance | Typical time in salt spray (ASTM B117) | Consequence |
| Pit initiation | Small dark spot on chrome | 200 – 500 hours | Cosmetic only; seal not affected |
| Pit growth | Visible pit, 0.1 – 0.3 mm | 500 – 1,000 hours | Seal lip begins to wear |
| Crack initiation | Hairline crack at pit edge | 1,000 – 1,500 hours | Seal leakage begins |
| Spalling | Chrome flaking, rough surface | 1,500 – 2,000 hours | Rapid seal failure, rod replacement required |
Raydafon Technology Group Co.,Limited has analyzed failed Hydraulic Lift Cylinder rods from field returns. The data shows that the average time to spalling in a coastal environment is 18 to 24 months for a standard chrome plated rod. With an advanced surface treatment, the time to spalling can be extended to 5 years or more.
2. How Does Chrome Plating Protect the Rod and Where Does It Fail?
Chrome plating is the most common surface treatment for Hydraulic Lift Cylinder rods. It provides a hard, low-friction surface that resists abrasion and corrosion. The chrome layer is typically 0.02 to 0.05 mm thick. It is applied by electroplating, which produces a micro-cracked structure. The micro-cracks are not a defect; they are a necessary feature that allows the chrome to relieve internal stress. However, the micro-cracks also provide a path for corrosive fluids to reach the underlying steel. If the steel is not properly protected, corrosion can initiate at the base of the micro-cracks and spread laterally, causing the chrome to lift. The table below shows the effect of chrome thickness and micro-crack density on corrosion resistance.
| Chrome thickness (mm) | Micro-crack density (cracks/cm) | Salt spray resistance (hours to pit) | Typical application |
| 0.02 | 400 – 600 | 200 – 300 | Indoor, dry environments |
| 0.03 | 200 – 400 | 300 – 500 | General outdoor |
| 0.05 | 100 – 200 | 500 – 800 | Coastal, humid |
| 0.05 + nickel underlayer | 100 – 200 | 1,000 – 1,500 | Severe corrosion |
In our factory, we apply a nickel underlayer before chrome plating for rods that will be used in coastal or chemical environments. The nickel layer acts as a barrier that prevents the corrosive fluid from reaching the steel even if the chrome layer is damaged. This duplex coating extends the time to pit initiation by 2 to 3 times.
3. What Alternative Surface Treatments Offer Better Corrosion Resistance?
There are three alternative surface treatments that offer better corrosion resistance than standard chrome plating. The first is electroless nickel plating with a high phosphorus content. This coating is uniform, even on complex shapes, and it provides excellent corrosion resistance in alkaline and neutral environments. The second is ceramic coating, such as chromium oxide or titanium nitride. These coatings are harder than chrome and more resistant to abrasion, but they are more expensive and require specialized equipment. The third is thermal spray coatings, such as tungsten carbide or aluminum oxide. These coatings are applied by spraying molten particles onto the surface. They are thick (0.1 to 0.5 mm) and provide excellent wear and corrosion resistance. The table below compares these treatments.
| Treatment | Thickness (mm) | Hardness (HV) | Salt spray resistance (hours) | Relative cost |
| Standard chrome | 0.02 – 0.05 | 800 – 1,000 | 200 – 800 | 1.0x |
| Nickel + chrome duplex | 0.03 + 0.03 | 700 – 900 | 1,000 – 1,500 | 1.5x |
| Electroless nickel (high P) | 0.02 – 0.05 | 500 – 600 | 1,000 – 2,000 | 1.8x |
| Ceramic (Cr2O3) | 0.05 – 0.15 | 1,200 – 1,800 | 2,000 – 3,000 | 3.0x |
| Thermal spray (WC) | 0.10 – 0.30 | 1,000 – 1,400 | 3,000+ | 4.0x |
Raydafon Technology Group Co.,Limited offers all of these surface treatments. Our factory can recommend the optimal treatment based on the operating environment, the required service life, and the budget. For a typical coastal application, we recommend the nickel plus chrome duplex coating. For a chemical plant with acid exposure, we recommend the ceramic coating.
4. How Should Surface Treatment Quality Be Verified Before Installation?
Verification of surface treatment quality should include four checks. The first is thickness measurement. The coating thickness can be measured with a magnetic or eddy current gauge. The thickness should be within the specification at five points along the rod. The second is adhesion testing. A simple tape test or a bend test can reveal poor adhesion. The third is hardness testing. The hardness can be measured with a microhardness tester. The fourth is corrosion testing. A salt spray test according to ASTM B117 should be performed on a sample from the same batch. In our factory, we perform all four checks on every batch of rods. We also provide a test certificate with the results.
Field verification tip: Before installing a Hydraulic Lift Cylinder, inspect the rod surface under a bright light. Look for any dull spots, discolorations, or small pits. A high-quality coating should be uniform and bright. If you see any defects, reject the cylinder and request a replacement.
Frequently Asked Questions About Hydraulic Cylinder Surface Treatment
Summary for Maintenance and Reliability Engineers
Surface treatment is the primary defense against corrosion on a Hydraulic Lift Cylinder rod. Standard chrome plating provides adequate protection for indoor and mild outdoor environments. For coastal, humid, or chemical environments, a duplex coating with a nickel underlayer or a ceramic coating provides significantly better corrosion resistance. The quality of the surface treatment should be verified by thickness, adhesion, hardness, and salt spray testing before installation. Raydafon Technology Group Co.,Limited has been manufacturing hydraulic lift cylinder units for over 20 years and provides a full range of surface treatment options for demanding applications.
Raydafon Technology Group Co.,Limited manufactures hydraulic lift cylinder units with hard chrome, nickel-chrome duplex, and ceramic coatings. We provide test certificates and surface roughness data for all of our products.
